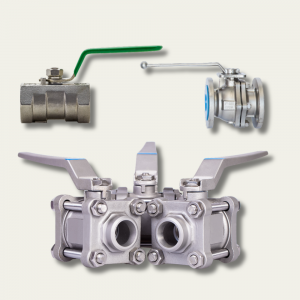
In the rapidly evolving landscape of industrial automation and fluid control systems, the role of valves is pivotal. Among these, motorized ball valves are emerging as a critical component due to their efficiency, reliability, and precision. These valves are increasingly becoming the preferred choice across various industries for controlling the flow of liquids and gases. This article delves into the multifaceted benefits of motorized ball valves, highlighting their role in enhancing operational efficiencies and offering insights into their applications across different sectors.
Understanding Motorized Ball Valves
Motorized ball valves are equipped with an electric actuator that facilitates remote control and automation of valve operations. This integration of technology allows for seamless operations, which is particularly beneficial in industries where precision and control are paramount.
Key Features
- Automation: Integrates seamlessly with automated systems, reducing the need for manual intervention.
- Precision: Offers precise control over fluid flow, essential for sensitive industrial processes.
- Durability: Constructed with robust materials to withstand harsh industrial environments.
Motorized ball valves are designed to offer superior control and are often preferred for applications that demand high reliability and precision. Explore advanced guides and tips on selecting the right motorized ball valve for specific industrial needs.
Benefits of Motorized Ball Valves
Motorized ball valves provide a range of benefits that enhance operational efficiencies and contribute to cost savings. Below are some of the key advantages:
Efficiency and Cost-effectiveness
- Reduced Energy Consumption: The efficient design minimizes energy use, leading to cost savings.
- Lower Maintenance Costs: Automated operation reduces wear and tear, extending valve life and decreasing maintenance needs.
For industries looking to optimize their operational costs, discover expert strategies here to implement motorized ball valves effectively.
Enhanced Safety and Reliability
- Remote Operation: Allows for safe control of the valve in hazardous environments, protecting personnel from exposure.
- Consistent Performance: Ensures reliable operation even under variable conditions, maintaining safety standards.
This reliability is critical in sectors such as chemical processing and oil and gas, where safety and consistency are of utmost importance. Learn about our tailored solutions for enhancing safety with motorized ball valves.
Applications Across Industries
Motorized ball valves are not confined to a single industry; their applications span multiple sectors due to their versatility and robustness.
Industrial and Commercial Applications
- Water Treatment: Used for controlling the flow of water in treatment plants, ensuring precise regulation.
- HVAC Systems: Critical in heating, ventilation, and air conditioning systems for regulating fluids.
- Food and Beverage: Ensures hygiene and precision in controlling liquid flows during processing.
For a comprehensive understanding of applications, find out more about this approach to integrating motorized ball valves in various industries.
Conclusion
Motorized ball valves represent a significant advancement in valve technology, offering a blend of efficiency, reliability, and precision. Their application across diverse industries underscores their versatility and essential role in modern industrial operations. As industries continue to seek ways to enhance efficiency and safety, the adoption of motorized ball valves is set to increase, driven by the need for automation and precise control. For further insights into how motorized ball valves can transform your operational processes, explore advanced guides and tips available online.
About the Author